Serious About Difficult Science. Built to Scale With You.
Delivering complex molecules from development to commercial manufacture requires more than capacity. It requires the right facilities, technologies and expertise working together to overcome scientific and manufacturing challenges at every stage of the drug development lifecycle.
Almac Sciences has invested in an integrated network of development and manufacturing facilities across the UK and Ireland supporting advanced intermediates, regulatory starting materials, Active Pharmaceutical Ingredients (APIs), highly potent compounds, peptides, radiolabelled compounds and specialised chemistry programmes.
Supporting the Complete Development Journey
From the first grams produced in the laboratory through to commercial-scale manufacture, our facilities are designed to provide scientific continuity and a clear pathway for scale-up.
Craigavon, UK: API Development & GMP Manufacture
Our Craigavon facilities provide integrated development and GMP manufacturing capabilities for small molecules, highly potent compounds and peptides.
Capabilities include:
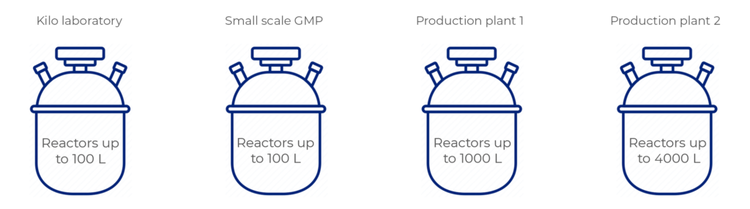
- Laboratory reactors from 250 mL to 20 L
- Kilo laboratory infrastructure from 50 L to 100 L
- GMP manufacturing reactors from 100 L to 1,000 L
- Major expansion programme increasing reactor capacity to 4,000 L
- Commercial-scale manufacturing capability supporting 200-300 kg batch sizes
- Dedicated highly potent API containment facilities
- GMP peptide development and manufacturing suites
- Integrated analytical and quality support
The Craigavon site serves as a centre of excellence for late-phase development and commercial API production, supported by extensive regulatory inspection history and proven GMP compliance.
Athlone, Ireland: Advanced Intermediates & Manufacturing Scale-Up
Almac Sciences Athlone provides specialised development and manufacturing capabilities for advanced intermediates, regulatory starting materials and commercial supply programmes.
Capabilities include:
- Development and pilot-scale reactors from 10 L to 1,000 L
- Manufacturing assets up to 8,000 L
- Approximately 90 m³ of manufacturing capacity
- Glass-lined, Hastelloy and stainless-steel reactors
- Supply capabilities ranging from kilograms to tens of tonnes
- Specialised distillation and purification technologies
- Multi-purpose chemistry infrastructure supporting complex synthetic routes
The facility provides strategic support for clients requiring secure and scalable supply chains for advanced intermediates and registered starting materials.
Advanced Technology Platforms
Difficult science often requires specialised technologies not commonly available within traditional manufacturing environments.
Our facilities support:
- Enzyme screening and optimisation
- Enzyme immobilisation
- Fermentation scale-up
- Bulk enzyme manufacture and supply
- Oligonucleotide synthesis support through specialist enzyme panels
- Cryogenic processing to -80°C
- High-temperature processing up to 220°C
- High-pressure operations up to 100 bar hydrogen
- cGMP flow hydrogenation
- Photochemistry capabilities
- Thin-film distillation
- Short-path distillation
- Falling-film distillation
- High-vacuum operation down to 1 mbar
These technologies allow our scientists to develop efficient and scalable manufacturing solutions for challenging molecules and processes.
Quality Built Into Every Facility
Our manufacturing network operates within a robust quality framework supported by FDA and MHRA inspection history, global quality systems and extensive regulatory experience.
With more than 30 Drug Master Files and a long-standing track record supporting global development and commercial programmes, clients can be confident their products are being developed and manufactured to the highest standards.
Serious About Difficult Science. Designed for Commercial Success.